Mild-Heat Evaporative System
Mild-Heat Evaporative & Drying System
RED Mild-Heat Evaporative & Drying System
RED System is designed for continuous concentration and solidification of brine, chemical effluent, high-organic effluent, and evaporation mother liquor.
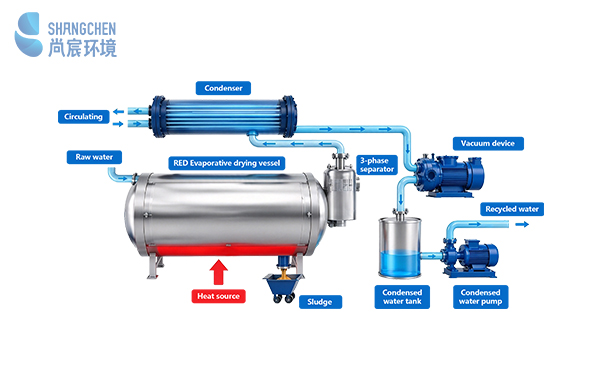
Proprietary evaporation drying kettle design suppresses scaling, coking, and blockage, ensuring easy cleaning. The system combines evaporation, drying, and sludge discharge. It can directly produce solid residue without additional crystallizers, dryers, and centrifuges.
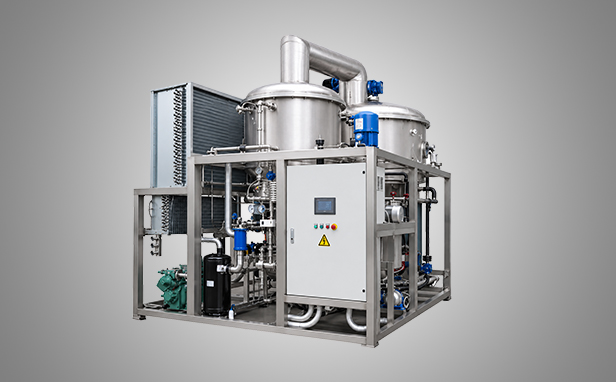
It supports vapor, heat water, or thermal fluid as heating media. Heat exchange occurs through the jacket and rotating blades, ensuring efficient heat transfer and superior thermal utilization.
Mild-heat vacuum evaporation reduces the boiling-point of effluent, enabling efficient concentration and crystallization without direct greenhouse gas emissions.
Compact skid-mounted design for easy installation, with intelligent control and remote monitoring for reliable operation.
Applications
Applications: Volume reduction, concentration, and drying of brine, elevated-COD effluent across the chemical, electroplating, metallurgical, pharmaceutical, new energy, machining, and hazardous waste treatment industries.
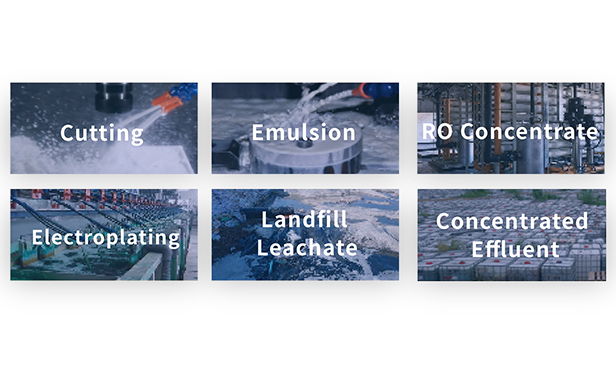
Typical Effluent: Cutting effluent, Emulsion effluent, landfill leachate, RO concentrate, and hazardous waste treatment effluents etc.
Product Model

SEV Mild-Heat Evaporative & Drying System
SEV system adopts vacuum evaporation and air-source heat recovery to achieve mild concentration and crystallization with reduced energy consumption and carbon emissions.
Its compact design minimizes space requirements and simplifies installation, enabling quick commissioning after connection to on-site wastewater lines, with intelligent controls for automated, unattended operation.
SEV system is suitable for treating emulsion effluent, cutting effluent, electroplating and coating effluent, cleaning effluent, and brine. It is ideal for low-volume effluent treatment in the electronics, electroplating, and machining industries.

Applications
SEV system is suitable for treating emulsion effluent, cutting effluent, electroplating and coating effluent, cleaning effluent, and brine. It is ideal for low-volume effluent treatment in the electronics, electroplating, and machining industries.
Product Features
Mild-Heat Evaporation
Operating under high vacuum, SEV system enables evaporation at 30–37°C, minimizing corrosion and making it suitable for heat-sensitive and scaling-prone materials.
Energy-Efficient
Depending on feed characteristics, effluent volume can be reduced by up to 90–97%. Heat pump technology enables efficient heat recovery, achieving a SMER of ≥4.0 kg H₂O/kWh.

Evaporation System for Complex Effluent
During zero liquid discharge (ZLD) and brine evaporation, impurities, high-boiling compounds, and organic matter accumulate in the mother liquor, compromising the crystal purity, crystallization, and MVR operating stability while promoting evaporator fouling.
SHANGCHEN’s proprietary evaporation technology offers a cost-effective, reliable solution for challenging waste liquid treatment.
The system is designed for elevated- Total Dissolved Solids (TDS>20%) and elevated-Chemical Oxygen Demand (COD>100,000 mg/L) effluent which typically characterized by aggressive corrosivity, elevated viscosity, and an elevated boiling point.
Product Solution
Complex waste liquid undergoes pretreatment to remove suspended solids, organics and other impurities before entering the evaporation system. Then the system recovers reusable water and produces crystals or residues through evaporation, concentration, crystallization, or drying.
Two solutions are available for treating complex effluent:
1. Crystallizable effluent: UltraMVR Evaporative System.
2. Other types of effluent: RED Mild-Heat Evaporative & Drying System.
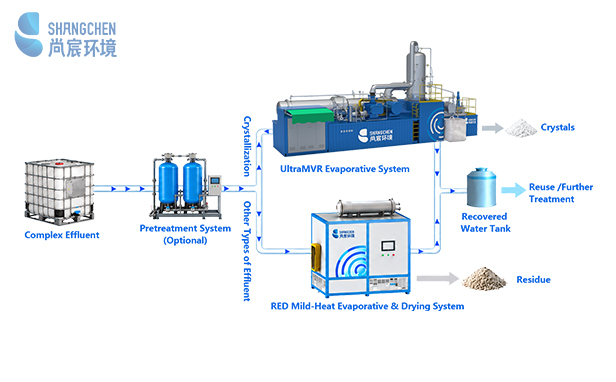
UltraMVR Evaporative System
Built on the ModMVR system, it raises the temperature of secondary steam to 60°C with proprietary MVR technology, enabling efficient concentration and crystallization of high-boiling waste liquids.
● Enhanced evaporation performance: Secondary steam of 60°C temperature enables efficient treatment of high-boiling-point, highly concentrated liquids, helping prevent low evaporation rates, compressor surging, and poor crystallization.
● Energy savings: HRMVR technology reduces operating costs to RMB 50–80 per ton of water evaporated.
● Durability and reliability: Titanium alloy and other corrosion-resistant materials ensure long service life and stable operation.
RED Mild-Heat Evaporative & Drying System
RED utilizes advanced low-temperature vacuum distillation technology to achieve efficient concentration and solidification of complex waste liquids characterized by poor crystallization behavior, high coking tendency, and low fluidity.
● Proprietary evaporation drying kettle design suppresses scaling, coking, and blockage, ensuring easy cleaning.
● The system combines evaporation, drying, and sludge discharge. It can directly produce solid residue without additional crystallizers, dryers, and centrifuges.
● It supports vapor, heat water, or thermal fluid as heating media. Heat exchange occurs through the jacket and rotating blades, ensuring efficient heat transfer and superior thermal utilization.
● The skid-mounted integrated is designed with a compact footprint. The system supports intelligent monitoring, remote control, and diagnostic functions, ensuring stable and reliable operation.
Evaporation System for Industrial Effluent
The system for industrial effluent is based on the SEV Mild-Heat Evaporative & Drying System. It achieves mild concentration of emulsions, cutting fluids, and other industrial effluents through vacuum low-temperature evaporation and condensation. By integrating air-source heat pump technology for heat recovery, the system significantly reduces energy consumption and delivers an energy-efficient, low-carbon solution.
Product Solution
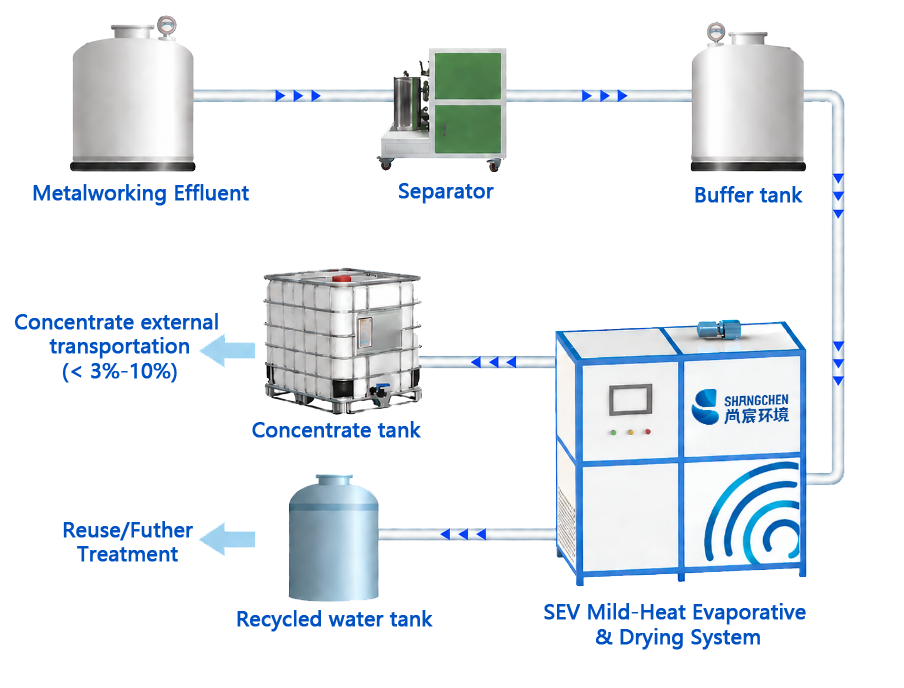
The industrial effluent is fed into the separator to remove grease, suspended matter and other substances, and then is absorbed into the SEV Evaporation System after flowing through a buffer tank. After low-temperature evaporation and deep concentration, ultimately produces reclaimed water and a minimal amount of concentrate.
Applications
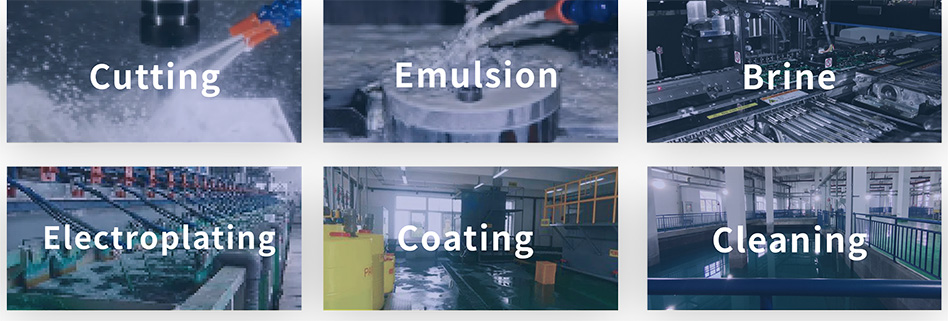
The system is suitable for the treatment of a wide range of industrial effluents, such as cutting fluids, emulsions, coating effluents, cleaning effluents, electroplating effluents, quenching effluents, casting effluents, metal-containing effluents, degreasing effluents, and other similar applications.
Product Features
Mild Temperature Evaporation
The system operates under a vacuum environment, enabling effluent evaporation at mild temperatures below 37°C. This low-temperature evaporation process significantly reduces equipment corrosion and is particularly suitable for heat-sensitive materials and effluents prone to scaling.
Deep Concentration
Based on the characteristics of different effluents, the system can achieve up to 90%-97% volume reduction by removing moisture, significantly reducing disposal costs and improving treatment efficiency.
Energy-Efficient
Equipped with advanced heat pump technology, the system efficiently recovers and reuses heat energy. The comprehensive moisture extraction ratio (SMER) can exceed 4.0 kg H₂O/kWh, delivering excellent energy efficiency.
Intelligent Control
Compact design with a small footprint. The system delivers intuitive operation, fully automated control, and unattended operation for reliable and efficient performance.
Guangdong Shangchen Environmental Technology Co., Ltd. is a large-scale technology-based comprehensive service provider of resource recycling. Shangchen is devoted to the field of industrial wastewater and has become a leading role in the industry after more than ten years of rapid development. The core business of the Company is concentrated in the field of industrial wastewater treatment, and covers pollution control fields such as river management, pyrolysis of domestic waste, heavy metal soil management, sludge reduction, waste acid and alkali recovery, and hazardous waste treatment. Shangchen is committed to providing customers with professional overall solutions, and has now formed a complete industrial chain of environmental pollution control throughout the entire life 。
1、Spent Alkali Recovery Equipment
2、Spent Acid Recovery Equipment
3、SDL&SDP Sludge Drying System
4、Mild-Heat Evaporative System
5、MVR Evaporative System
6、Membrane Concentration System